Industrial Borosilicate Solvent Recovery Plants
Solvents represent one of the most substantial operating expenditures in fine chemical synthesis, pharmaceutical manufacturing, botanical processing, and specialty coatings. Spent solvents—such as acetone, methanol, isopropanol (IPA), ethanol, dichloromethane (DCM), tetrahydrofuran (THF), toluene, and ethyl acetate—frequently contain active ingredients, dissolved polymers, particulate resins, and dissolved salts that render them unusable without purification.
Goel Glass designs, fabricates, and commissions turnkey Borosilicate Glass Solvent Recovery Plants capable of reclaiming valuable process solvents with recovery yields up to 98% and purity levels conforming to virgin solvent specifications. Fabricated from thermal shock resistant Borosilicate Glass 3.3 and virgin PTFE, these systems eliminate metal leaching and corrosion from aggressive halide or acidic residues.
Continuous Recovery Advantages
- Steady-State Thermodynamic Balance: Continuous automated feed metering and constant reboiler load.
- Minimized Energy Consumption: Thermal integration utilizes incoming raw feed to precool overhead condensates.
- Continuous Bottom Residue Blowdown: Eliminates reboiler downtime for cleaning and discharge.
- Zero-Emission Vent Scrubbing: Secondary chilled-water vent condensers prevent VOC loss into atmosphere.
Custom Engineering Capacities
- Capacity Range: Scalable configurations from 20 L/hr pilot skids to multi-ton per day commercial units.
- Vacuum Systems: Deep vacuum packages for low-boiling heat-sensitive solvents.
- Instrumentation: Digital thermal sensors, explosion-proof pumps, and automatic reflux ratio controllers.
- Skid Mounting: Pre-assembled on 304/316 Stainless Steel modular frame structures.
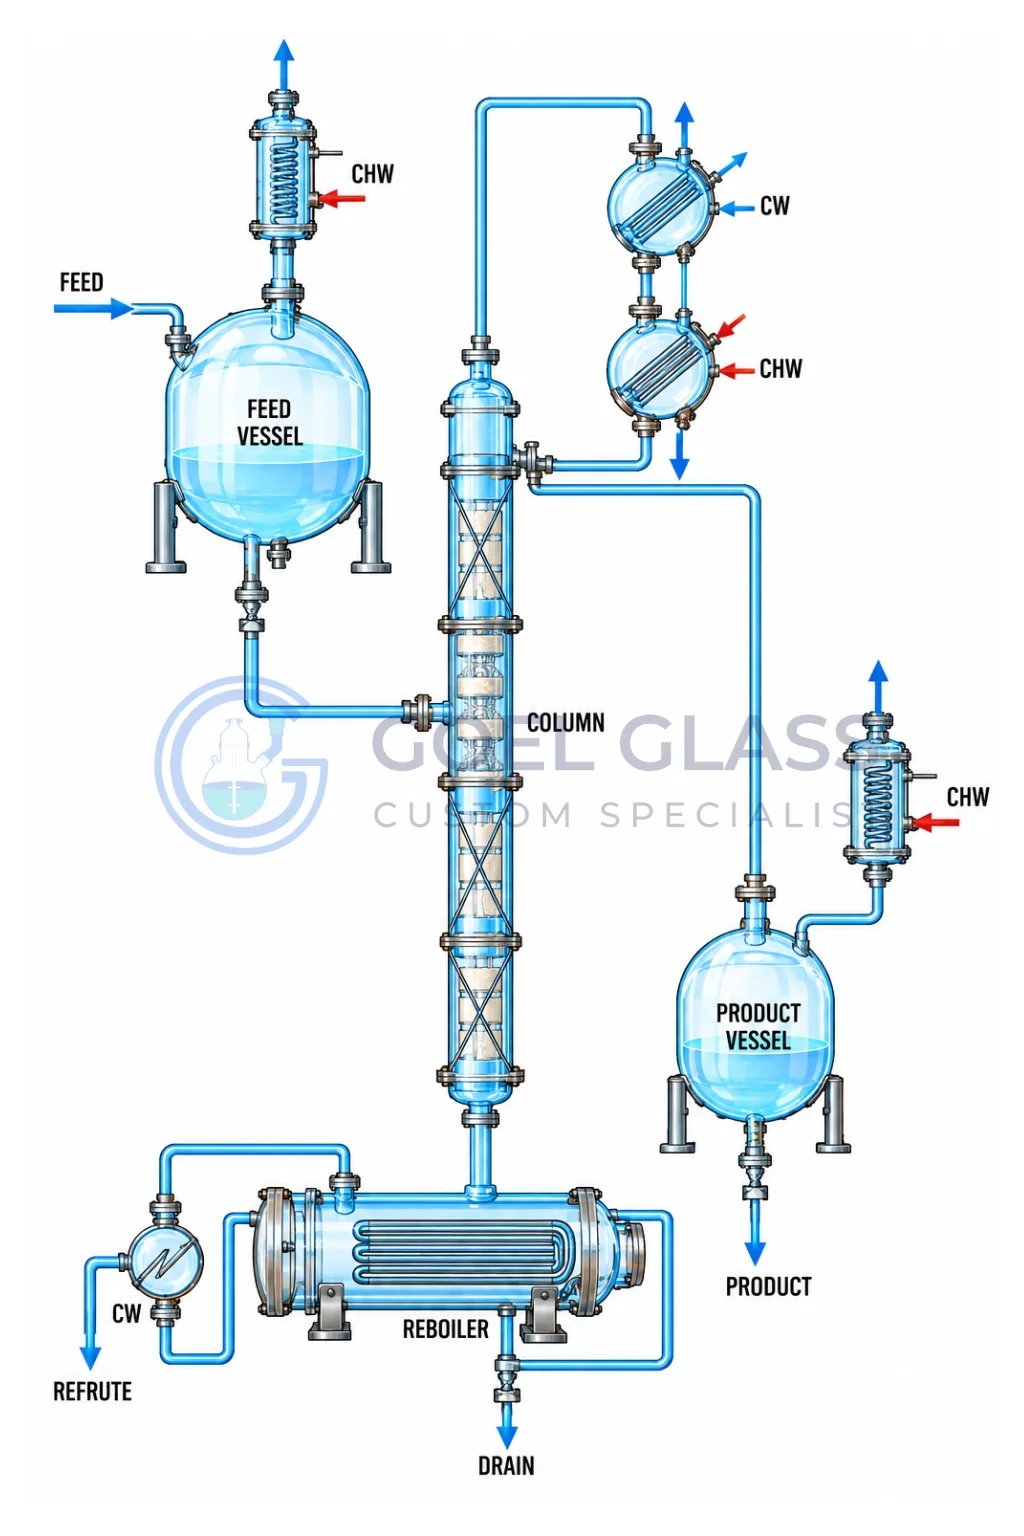
Key Engineering Features
- Primary & Secondary Condensation: Dual-stage shell & coil condensers with glycol chilling.
- Automatic Reflux Splitting: Electromagnetic divider delivers sharp fractions for solvent binary mixtures.
- Explosion-Proof Compliance: Compatible with Class 1, Div 1 / ATEX Zone 1 flammable solvent processing.
- High Return on Investment: Typically achieves capital payback within 3 to 6 months of commissioning.
Industrial Applications
- Pharmaceutical Manufacturing: Reclamation of reaction and washing solvents (IPA, Acetonitrile, Methanol).
- Botanical & Essential Oil Refineries: Pure ethanol recycling following biomass percolation and winterization.
- Paints, Inks & Coatings: Recovery of xylene, toluene, MEK, and butyl acetate from wash streams.
- Fine Chemical Syntheses: Continuous stripping of reaction mediums to drive condensation reactions.